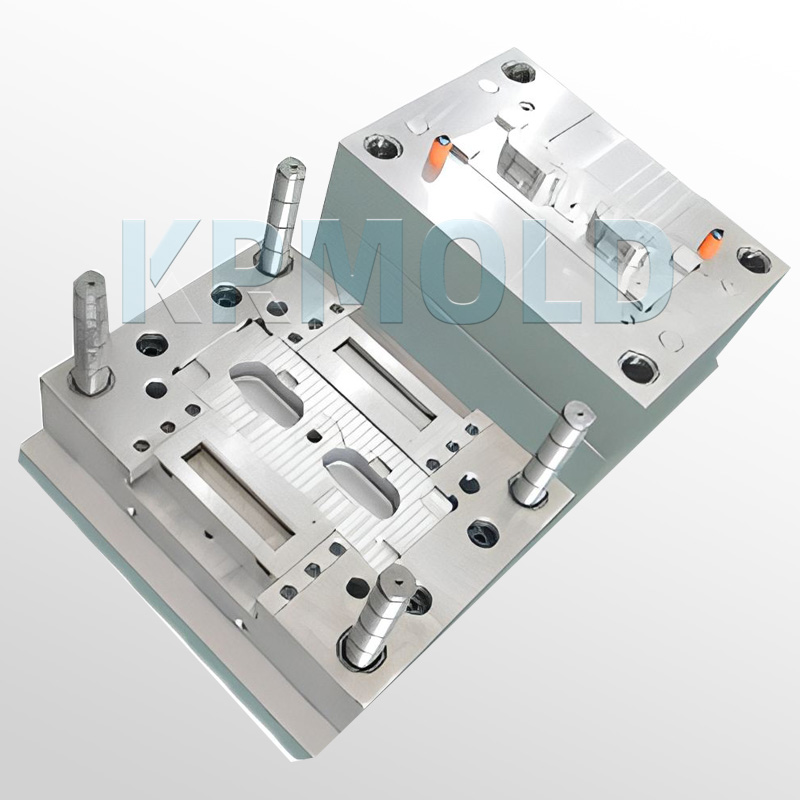
Introduction to Bluetooth Earphone Housing Mold
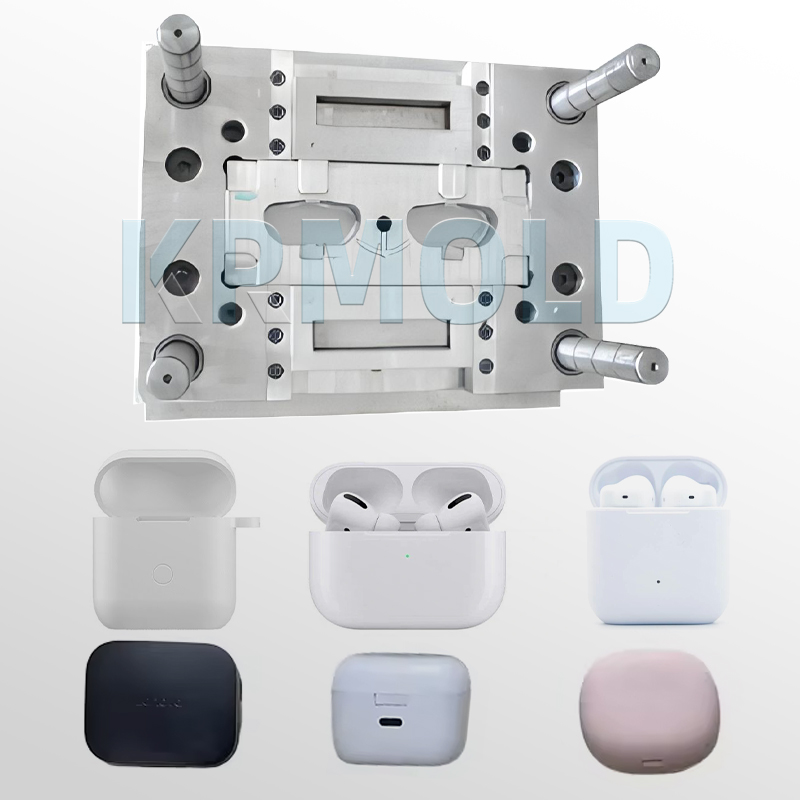
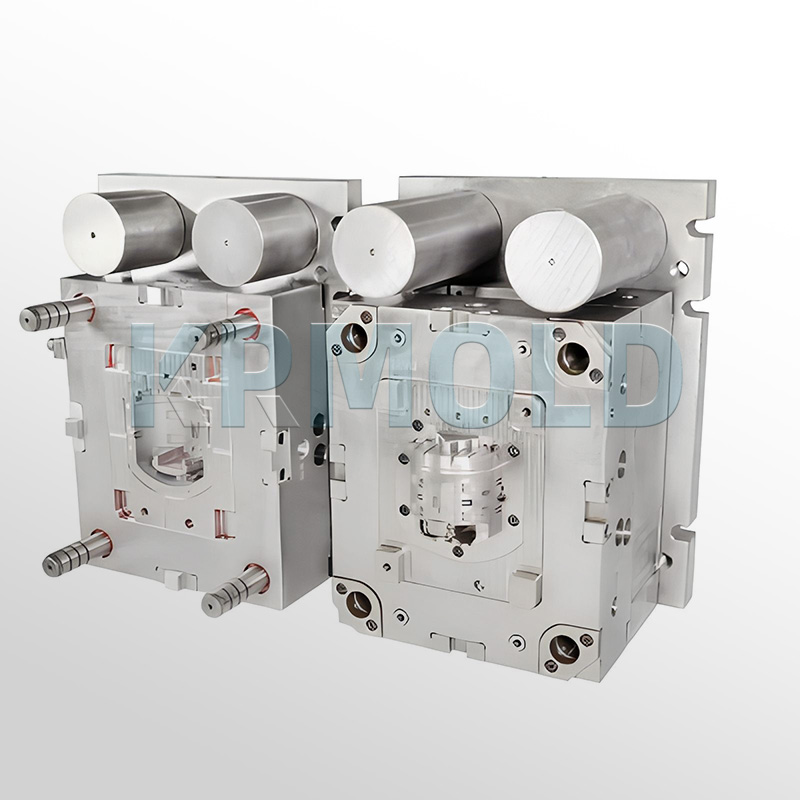
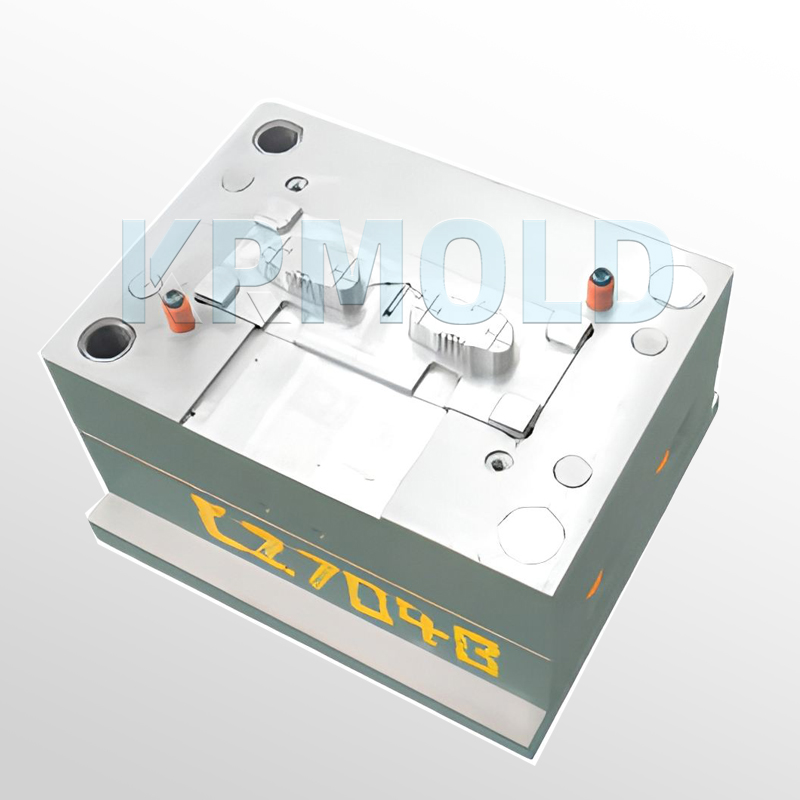
The Bluetooth earphone housing mold—also known as a wireless Bluetooth earphone case mold or TWS charging case mold—is custom-designed specifically for the external casings of Bluetooth earphones and their charging compartments; it serves as core tooling equipment in the manufacturing process.
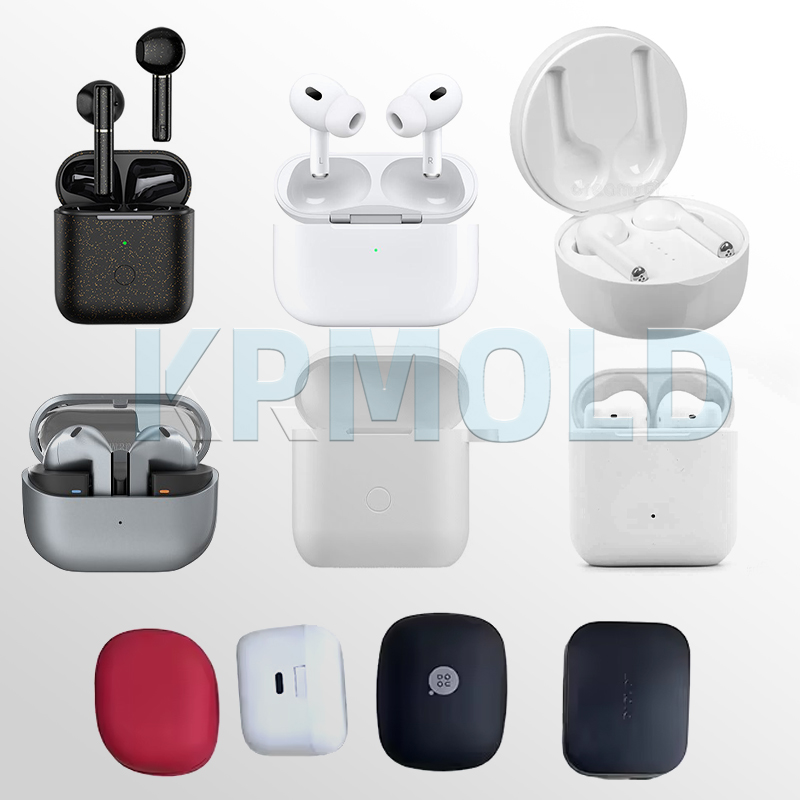
These Bluetooth earphone shell molds are compatible with various sizes and styles of products, such as TWS Bluetooth earphones and wireless in-ear models, precisely meeting the molding requirements for both the earphone storage housing and the charging case.
KRMOLD offers custom Bluetooth earphone housing mold solutions featuring diverse structures, specifications, and manufacturing processes, ensuring full compatibility with Bluetooth earphone products across a wide range of colors, sizes, and functional configurations.
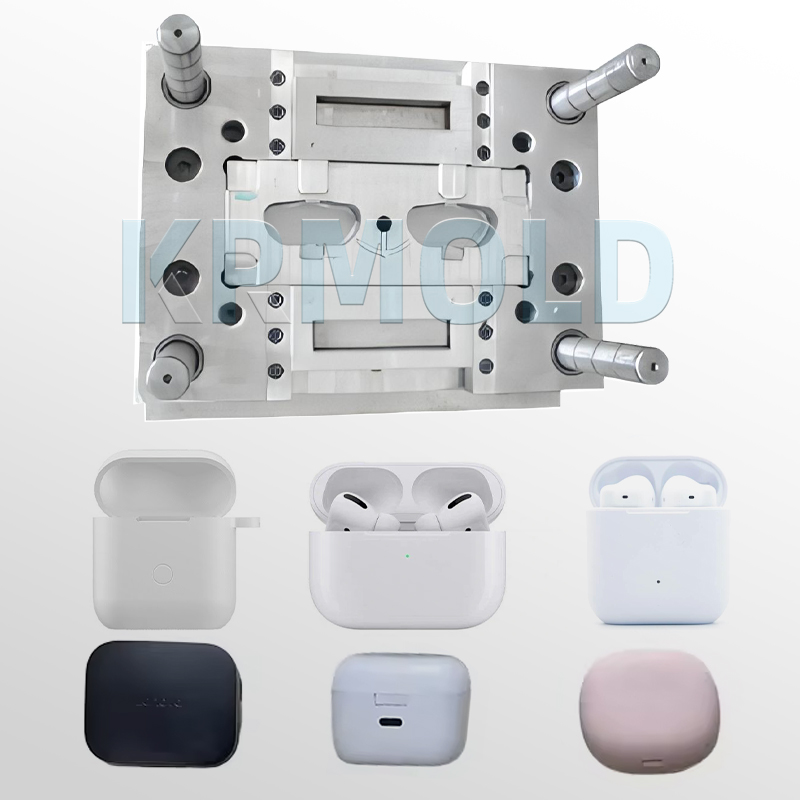
Specifications of Bluetooth Earphone Housing Mold
| Mould Material | PS, ABS,PP, PVC,PMMA,PBT,PC, POM,PA66,PA6,PBT+GF,PC/ABS,PEEK,HDPE,TPU,PET,PPO,etc |
| Standard | LKM/HASCO/DME/FUTA,etc |
Design Software | UG,Pro-E |
| Mould Base | P20 , 45# , 4CR13 , etc; |
| Runner | Cold/Hot Runner |
| Mould Material | P20,P20H, 718, 718H,2738, Nak80, S136, SKD61,8407,H13, 2343,2344,2311,2312,2379,2316,2093,2767,etc |
| Cavity | Single/Multi Cavities |
| Surface | heat treatment,polishing, texture,coating,etc |
| Mould Life | 0.5-500 million Shots |
| Specification | Customized |
| Gate | Side gate, Edge gate, Submarine, Pin Point, Horn, Directe gate,Capillar, etc, |
Advantages of KRMOLD Bluetooth Earphone Housing Mold Design
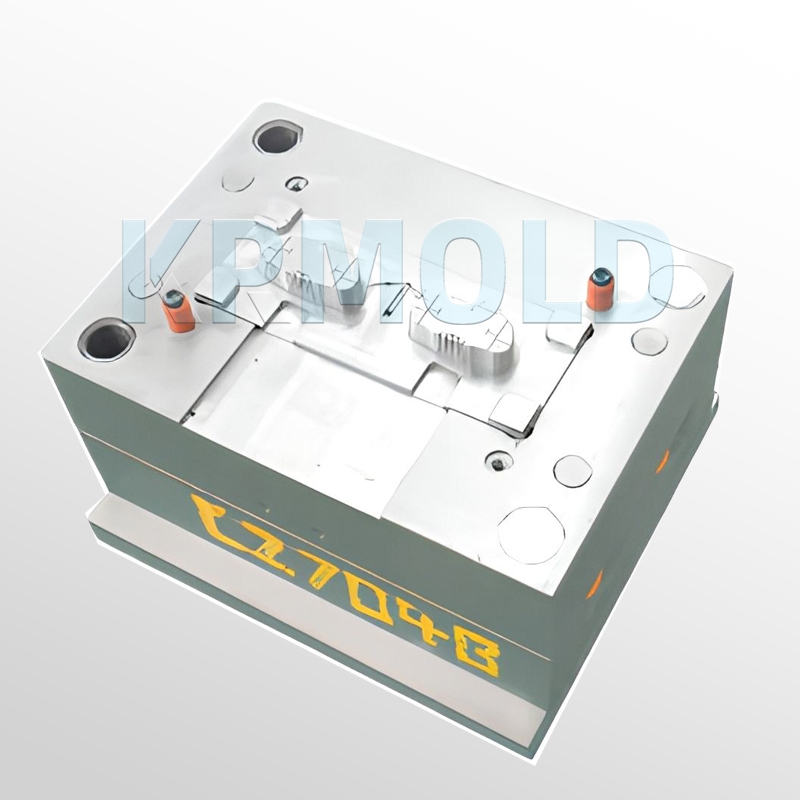
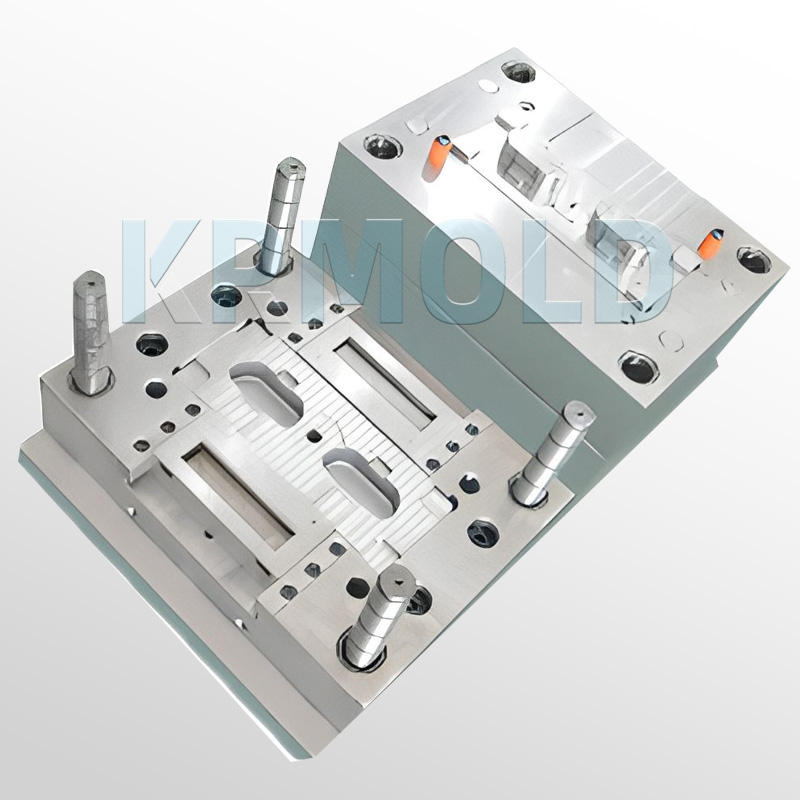
Precision Parting Line & Complex Surface Design
During the design phase of the TWS charging case mold, KRMOLD focuses on optimizing precision parting lines and complex surface structures. We precisely position the parting lines for wireless Bluetooth earphone case molds.
Addressing the two primary parting structures—flat surfaces and complex curved surfaces—we meticulously design interlocking features (such as steps and counter-steps) and strictly control mating clearances within the 0.05mm standard. This fundamentally prevents defects like housing misalignment, uneven seams, and sharp edges, ensuring a flush, seamless fit between the upper and lower shells.
Bluetooth earphone housings often feature streamlined, high-gloss curved surfaces, thin walls, and intricate internal structures. KRMOLD optimizes the Bluetooth earphone housing mold's demolding mechanism by precisely setting draft angles between 0.5° and 1°, ensuring smooth part ejection while preserving the smooth, rounded quality of the curved surfaces.
For intricate internal features—such as snap-fits, reinforcing ribs, magnet slots, and charging alignment slots—we employ ultra-high machining precision (at the 0.01mm level) to perfectly replicate the design, meeting the exacting assembly requirements of Bluetooth earphone housings.
Two-Color/Multi-Material Injection Molding Process Design
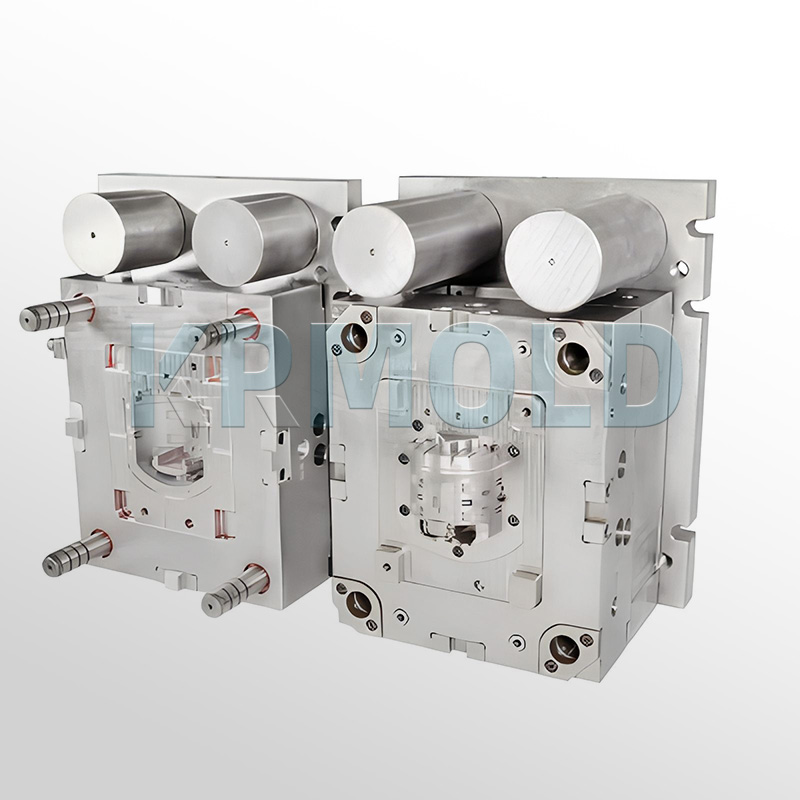
KRMOLD specifically optimizes the mold structure for two-color and multi-material injection molding. Compatible with mainstream material combinations—such as rigid PC+ABS and soft TPU—the wireless Bluetooth earphone case mold enables integrated injection molding that combines a rigid outer shell with soft, over-molded internal cushioning structures.
In the structural design, we precisely plan the injection sequence, pressure parameters, and over-molding zones. We also optimize mold alignment mechanisms to completely eliminate processing issues such as soft material flash, stringing, or delamination.
For critical areas like magnet slots, charging contacts, and fixed inserts, we design specialized local over-molding and insert molding configurations.
This ensures a tight bond between soft and hard materials and precise positioning of metal inserts, resulting in a more structurally robust and reliable final product.
Design Adapted for High-Gloss & Textured Surface Finishes
KRMOLD Bluetooth earphone shell molds are designed to accommodate a wide range of surface finishing requirements. For high-gloss product surfaces, the mold cavities undergo a high-precision mirror-polishing process using specialized fixtures.
This eliminates issues such as rounded cavity edges or uneven surface textures, resulting in Bluetooth earphone housings that are lustrous, translucent, and smooth to the touch—meeting high-end industry standards for aesthetics.
For areas requiring matte textures—such as the bottom casing and internal structural components—the TWS charging case mold supports precise machining of various textures, including EDM (spark) and laser patterns.
This ensures uniform texture and consistent quality across the molded product, fully satisfying customized aesthetic requirements.
Features of Bluetooth Earphone Housing Mold
1. High-Precision Tolerance Control KRMOLD strictly controls the dimensional accuracy and geometric tolerances of the Bluetooth earphone housing molds. Critical mating dimensions—such as the charging case lip clearance, earphone slots, and assembly alignment holes—are maintained within a tolerance of ±0.05mm, ensuring a precise fit between the housing, the earphone unit, and internal electronic components. Geometric tolerances, such as flatness and perpendicularity, are also rigorously controlled; for instance, the flatness error of the mating surfaces on the charging case is kept within 0.1mm, ensuring an excellent seal and a seamless, flush appearance when closed.
2. Premium Mold Materials All TWS charging case molds are constructed from high-quality mold steels—such as S136 and H13—known for their high strength, wear resistance, and polishability. These steels offer uniform hardness, excellent toughness, and superior resistance to corrosion and wear. This ensures long-term dimensional stability and significantly extends the wireless Bluetooth earphone case mold's service life, effectively reducing long-term replacement and maintenance costs for the customer. Additionally, specialized surface treatments—including mirror polishing, texturing, and hardening—are applied to the mold cavities based on specific process requirements, further enhancing smooth part ejection and surface finish quality.
3. High Production Efficiency KRMOLD Bluetooth earphone shell molds feature a lightweight, standardized structural design. Equipped with integrated automatic ejection and demolding mechanisms, they are perfectly compatible with automated injection molding lines, significantly boosting mass production efficiency. We offer flexible customization options—such as 1-cavity, 2-cavity, or 4-cavity configurations—tailored to your specific production requirements and injection molding machine tonnage. | 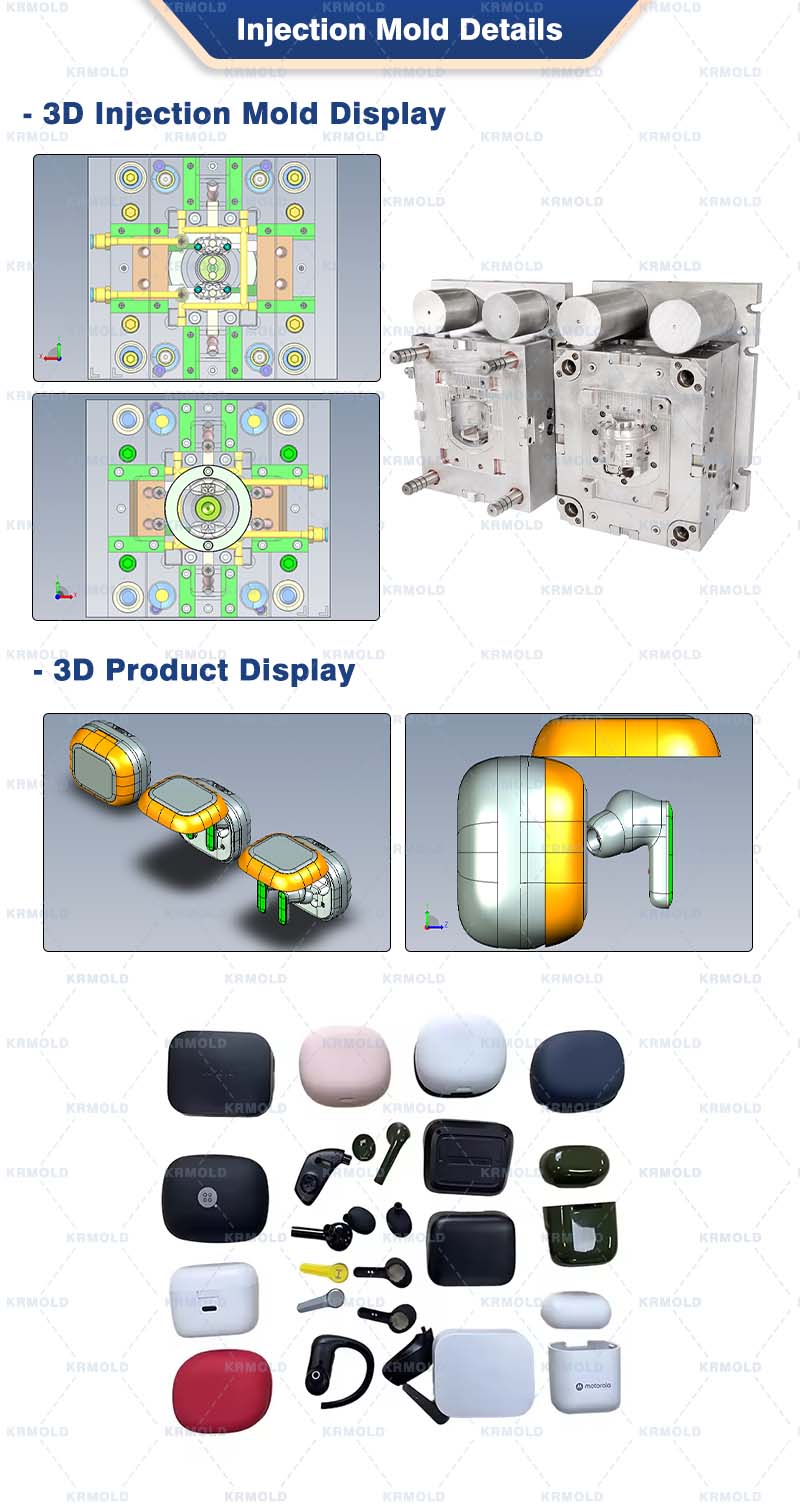 |
Why Choose KRMOLD?
Efficient and Reliable Lead Times
KRMOLD operates a standardized TWS charging case mold manufacturing facility equipped with a full suite of processing machinery. We can handle multiple simultaneous custom orders for wireless Bluetooth earphone case molds, managing the R&D and production of both standard injection molds for Bluetooth earphone housings and precision overmolding tools. Our substantial production capacity ensures we can strictly meet even the tightest delivery schedules.
Comprehensive Quality Control System
We maintain a rigorous end-to-end quality inspection system (covering IQC, IPQC, FQC, and OQC). Every TWS charging case mold undergoes comprehensive testing—from raw materials and the machining process to the finished product—ensuring strict control over precision and quality. We also offer customized pre-shipment inspections and dedicated QA after-sales support to meet specific client needs.
Extensive Expertise in Complex Manufacturing Processes
With years of specialization in insert molding and multi-material overmolding, KRMOLD has accumulated a wealth of proven experience in designing and manufacturing complex, thin-walled, and high-precision wireless Bluetooth earphone case molds.
Custom Bluetooth Earphone Housing Mold Manufacturing Process
KRMOLD provides a streamlined, one-stop customization service for Bluetooth earphone housing molds:
Client Consultation → Precise Requirement Confirmation → Receipt of Product Drawings/Samples → Mold Structure Design → Prototyping/Sampling → Sample Approval → Mass Production & Delivery → Comprehensive After-Sales Service
We employ a dedicated project customization model, ensuring every TWS charging case mold is precisely tailored to the client's project parameters and production needs.
By strictly managing every stage—from design and machining to mold trials and final delivery—we provide high-quality, perfectly matched Bluetooth earphone housing mold solutions.
Specify the type of plastic (e.g. PP, ABS) and post-processing requirements (e.g. spraying, silk-screen printing), and provide 2D or 3D plastic part drawings should be provided. At the same time, provide the production volume, appearance requirements, tolerance standards, etc.
Generally speaking, our engineers will start to prepare the quotation immediately after the customer provides the complete production requirements. Usually it takes about 1-3 days.
The lead time for regular injection molds is usually 30-60 days, and may be longer for complex molds. For example, the typical lead time for liquid silicone molds is around 60 days, covering design, manufacturing, mold testing, etc.
High-precision processing technology: High-precision equipment such as CNC machining centers (CNC) and electric discharge machining (EDM) are used to optimize the design process in combination with CAD/CAM software. Quality control: Inspection of key dimensions of the mold by Coordinate Measuring Machine (CMM) and verification of multiple sample batches during the trial molding stage. Material Selection: Use die steel with high wear resistance (e.g. H13, S136) and surface treatment (e.g. nitriding, chrome plating) for die nuts to extend the life.
After every 50,000 molds, check the guide pillar, ejector pin and other wear parts, and clean up the residual plastic and rust on the mold surface. Use high temperature grease for sliding parts (e.g. tilt top, slider) to reduce friction loss. Ensure that the water circuit is smooth and the temperature difference is ≤5℃ to avoid cracking of the mold due to thermal stress.
Mould cost of materials accounted for about 30-40% (such as 1 ton of P20 steel price of about 20,000 yuan), processing costs accounted for more than 50% (CNC labor hourly rate of about 80-150 yuan / hour). Small batch production can choose aluminum mold or simplify the structural design; more than 100,000 pieces is recommended to use carbide inserts to enhance life!
Mould injection products need to fully meet the design requirements (such as size, appearance), and can be continuous and stable production. Mold marking, inspection reports (such as material hardness test) and engineering drawings should be complete.
Mould steel (such as S136H, NAK80 and other imported materials cost more) and the type of mold embryo (aluminum mold short-term cost is low but short life) directly affect the cost, the use of CAD/CAE/CAM design technology, hot runner system, etc. will increase the upfront investment, but can enhance the long-term benefits (such as reducing the sprues, increase production capacity).